PVC flooring, pipes and profiles · Practical application guide
PVC products. Color & processing trials.
Keep PVC-resin phr separate from finished-compound percentages, and use distinct workflows for plastisols and thermoplastic compounds.
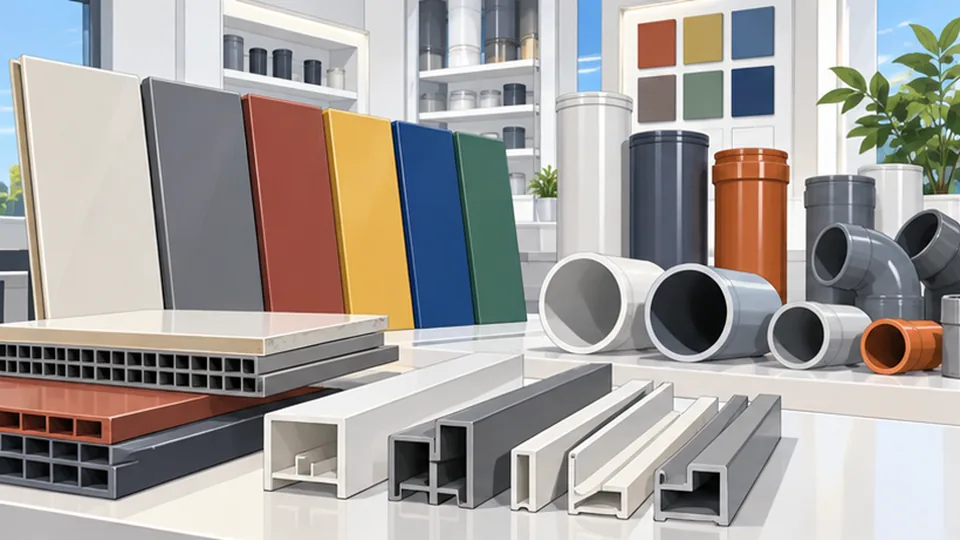
Separate the three processing routes
Identify a plastisol, a flexible compound for calendering/extrusion, or a rigid compound for pipes and profiles. Record resin, plasticizer, stabilizers, lubricants, fillers and rework. The material route determines how pigment is incorporated and what must be tested. BYK provides separate guidance for plastisols and compounds, while Baerlocher distinguishes their stabilizer requirements. Plastisol route; Compound route; Stabilizer selection
Do not adopt the same colorant carrier or dispersant addition merely because both products are called PVC. A fluid paste and a rigid profile need different process and finished-product checks.
Calculate colorant on the declared PVC-resin basis
Where the approved recipe uses phr, calculate on 100 parts PVC resin, not on the entire filled compound. Illustrative mass balance: a base recipe contains 100 parts PVC resin + 60 parts other approved ingredients. A chosen 2 phr pigment gives 162 total parts; pigment is 2/162 × 100 = 1.235% of the final compound. The 60-part balance and 2-phr target are arithmetic assumptions, not a proposed PVC formulation.
| Illustrative 10 kg PVC-resin basis | Mass |
|---|---|
| PVC resin | 10.00 kg |
| Existing other ingredients at 60 phr | 6.00 kg |
| Dry pigment at 2 phr | 0.20 kg |
| Resulting compound | 16.20 kg |
If that 200 g pigment is supplied in a documented 50% pigment paste, weigh 400 g paste and account for 200 g carrier. Do not deduct it from plasticizer unless its composition and role justify that adjustment. Total-solids percentage is not necessarily pigment percentage.
A sourced plastisol dispersant calculation
For DISPERPLAST-1150 in PVC plastisols, BYK gives 1–3% additive as supplied on inorganic pigment solids. This is an additive dose, not the amount of pigment in flooring. Organic pigments and fillers have their own entries; do not combine them casually. BYK PVC-plastisol dose table
For a separate screening charge containing 100 g inorganic pigment, calculated additive trials are 1 g, 2 g and 3 g. The middle point is an interpolated screening level. Disperse the additive into the suitable liquid components before incorporating solids, as its TDS directs. Keep the existing plasticizer and filler balance documented, and include a control.
The same TDS gives a different thermoplastics section for specified PE/PP/PET masterbatch routes. Do not use that section as a rigid-PVC processing instruction or transfer the water-only DISPERBYK-190 grind from paint manufacture into a plastisol.
Route A: make and evaluate the plastisol
- Weigh the approved resin/liquid components and prepare the color dispersion through the selected compatible route. Record addition order and temperature.
- Incorporate the colorant, controlling entrained air. Compare viscosity using the same test temperature and shear procedure; record both initial and stored values.
- Prepare the relevant flooring/coating layer with consistent thickness and backing. Follow its prescribed gelation/fusion cycle, recording the actual exposure.
- Inspect the finished layer for streaks, specks, bubbles and shade changes. If the product is multilayer, evaluate the completed stack and any contact-staining requirement.
Route B: process the dry blend or compound
- Use the approved hot/cool-mixing or compounding sequence. Calibrate pigment feeding and retain a reference from the same resin and stabilizer lots.
- Record actual thermal history and the established fusion/processing indicators, such as torque or pressure trends. Do not increase temperature blindly to remove color specks.
- Extrude or calender the intended geometry and separate start-up from stable production samples. For pipes or profiles, match color on the actual surface and thickness.
- Verify dimensions and specified mechanical/exposure properties before releasing the color. Keep stabilizer and lubricant adjustments traceable as separate formulation changes.
Troubleshooting and finished-product QC
| Observation | First checks | Next action |
|---|---|---|
| Plastisol viscosity rises | Dispersion, temperature, aging, additive compatibility | Compare control and candidate over agreed storage |
| Color drifts during extrusion | Dosing, residence, stabilizer system | Repeat a fixed-condition processing run |
| Specks or surface defects | Agglomerates, contamination, fusion | Inspect dispersion and process data |
| Contact staining | Pigment/paste carrier and plasticizer interactions | Run the application’s contact test |
Compare color after equivalent conditioning and use matching backing and surface texture. Add required heat-aging, weathering or migration testing for the finished product. A dark color must not be used to conceal processing damage. Drinking-water, indoor-air or other application approvals concern the actual formulation and final article, not a generic pigment label.
Prepare a useful grade request
Send FUXIN the PVC route, resin-based phr and total-formula ledger, target specimen, pigment/paste composition, processing history and defect photographs. Include the candidate results rather than only a desired color name.
Technical references
- BYK — PVC plastisols
- BYK — PVC compounds
- Baerlocher — PVC stabilizers
- BYK: DISPERPLAST-1150 TDS, PVC-plastisol and thermoplastics dose bases
Independent technical guidance used for this application overview. These references are not FUXIN project case studies or a substitute for a grade-specific technical data sheet.