Iron Oxide Pigment Storage Protects Powder Quality
Iron oxide pigment storage is an important part of maintaining material quality in concrete manufacturing, coatings production, and other industrial applications. Although iron oxide pigments are known for their chemical stability, improper storage conditions can affect powder handling, dispersion, and production efficiency.
Moisture exposure, damaged packaging, and cross-contamination are common problems that manufacturers and contractors should prevent through proper warehouse management.
Moisture Can Affect Pigment Powder Handling
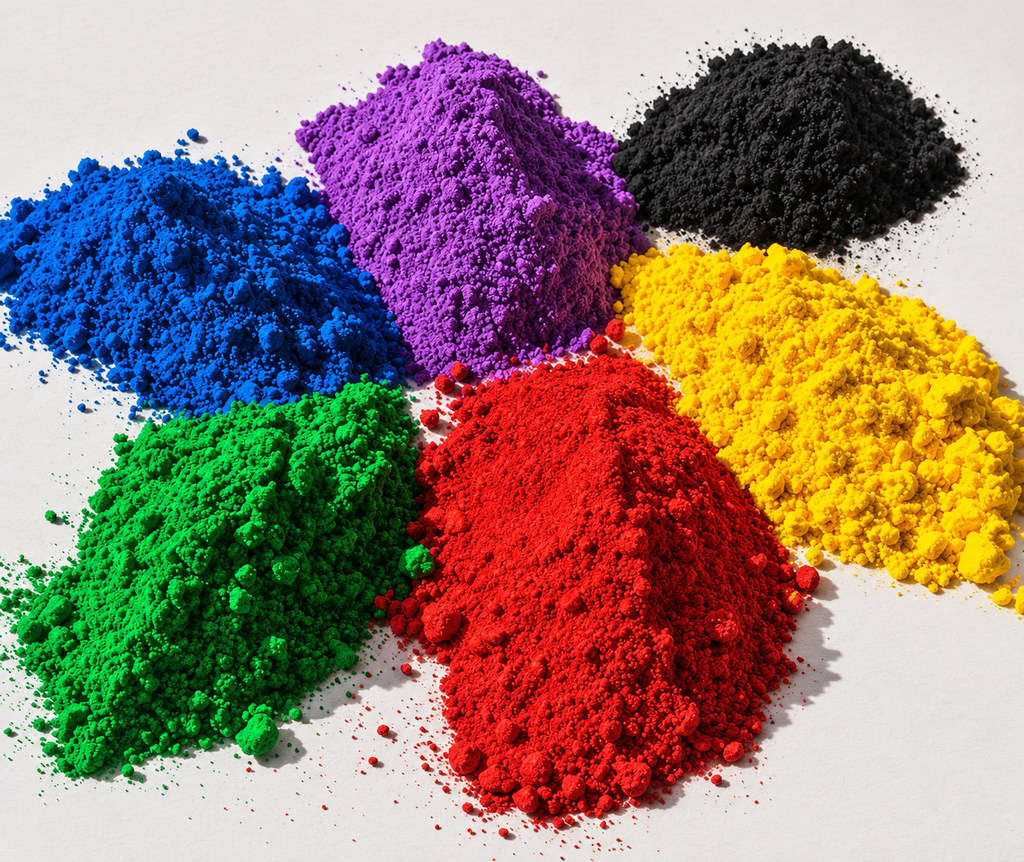
Iron oxide pigments are commonly supplied as fine powders or granulated materials. Their physical condition should remain suitable for accurate weighing, handling, and dispersion.
When pigment powder is exposed to moisture, it may develop lumps or become more difficult to discharge from packaging.
Moisture-related agglomeration can also complicate pigment distribution during production.
The severity of these problems depends on the pigment grade, moisture exposure, and storage conditions.
Maintaining a dry storage environment helps preserve the material’s handling characteristics.
Proper Packaging Reduces Contamination
Iron oxide pigments are frequently supplied in bags or bulk packaging designed for industrial transport and storage.
Packaging should remain intact until the material is required for production.
After opening, partially used bags should be securely closed to reduce moisture exposure and prevent contamination.
Damaged packaging should be inspected, and affected material should be transferred to a suitable clean container where appropriate.
Different pigment grades and colors should be stored separately to avoid accidental mixing.
Clear product labels help operators identify the correct material during production.
Warehouse Conditions Influence Storage Quality
Pigment storage areas should be protected from rainfall, excessive humidity, and extreme temperature fluctuations.
Bags should be placed on suitable pallets or storage racks rather than directly on damp warehouse floors.
Storage locations should remain clean and protected from water leakage.
Manufacturers should also avoid placing pigment packaging near incompatible materials or areas where accidental contamination may occur.
Temperature limits vary according to pigment composition and product grade. The manufacturer’s technical data sheet should determine the applicable storage requirements.
Pigment Lumps Require Inspection Before Use
Not every lump indicates that pigment has permanently lost its coloring properties.
Some loosely compacted powder may separate during normal handling, while hard or moisture-affected agglomerates require additional investigation.
Before using material that has developed significant lumps, operators should inspect the packaging condition and check for evidence of moisture contamination.
Where necessary, samples should be evaluated for dispersibility and coloring performance.
Mechanical screening or other processing should only be used when permitted by the supplier’s recommendations.
Material showing signs of contamination or deterioration should not automatically be returned to production.
Inventory Management Reduces Material Waste
Proper inventory management helps manufacturers maintain consistent pigment supplies.
Each batch should be clearly identified by product grade, color, production lot, and relevant storage information.
A first-in, first-out inventory system can help reduce unnecessary storage time.
Warehouse personnel should inspect older stock periodically, particularly when packaging has been opened or exposed to unsuitable conditions.
Before large-scale production, questionable material should be evaluated against the relevant product specifications.
The recommended storage period depends on the pigment formulation, packaging type, and manufacturer’s guidance.
Safe Handling Supports Production Efficiency
Fine pigment powders can generate airborne dust during weighing, transfer, and mixing.
Suitable dust extraction, housekeeping procedures, and personal protective equipment should be used according to the product’s safety data sheet.
Clean handling equipment also helps prevent contamination between different pigment colors.
For manufacturers using several pigment grades, dedicated or thoroughly cleaned equipment can reduce unintended color mixing.
Consistent Storage Supports Reliable Pigment Performance
Iron oxide pigment storage should be treated as part of the production quality management process.
Dry conditions, suitable packaging, clear identification, and regular inspection help maintain the physical condition of pigment powders.
These measures are especially important for manufacturers producing colored concrete blocks, paving stones, roofing tiles, and decorative construction materials.
By preventing avoidable moisture exposure and contamination, manufacturers can reduce material waste, support consistent pigment handling, and maintain more reliable production operations.
